
Introduction — a workshop morning, a hard number, a question
I remember walking into a sheet-metal shop one damp morning and seeing tooling racks piled high with one-off jigs. The owner told me they were burning 18% of production hours just swapping fixtures (that’s real waste). An industrial 3d printer sat in the corner — dusty, underused, and misunderstood. Recent industry data shows additive tool delivery can cut lead times by weeks and reduce scrap by double digits. So I ask: can distributed, on-demand tooling actually change how factories organize maintenance and spare parts?
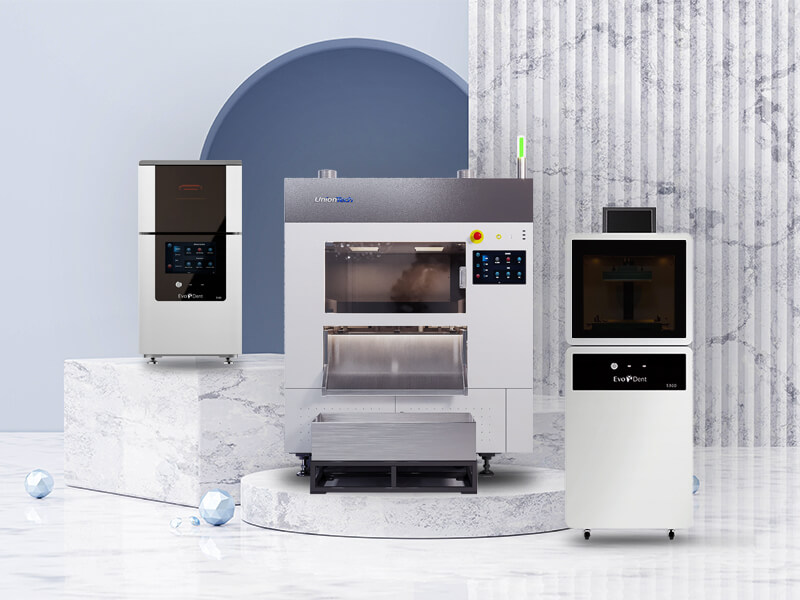
I write with a mix of concern and hard facts. I’ve spent over 18 years in industrial manufacturing and B2B supply chain work, and I’ve seen how small gains in tooling uptime translate directly to margin. The rest of this piece digs into what stops teams from adopting additively manufactured tooling, what hidden pains show up on the factory floor, and which practical signals suggest a real return-on-investment. (Yes — I’ve audited lines where a single failed fixture cost $12,400 in a single weekend.) Let’s look closer at the friction points and the real choices ahead.
Why current approaches fail: the flaws I keep seeing
industrial 3d printing company offerings promise speed, but experience tells a different story when old habits meet new tools. I’ll be technical here — surface finish, support structures, and post-processing often get glossed over in sales demos. In one case I oversaw in June 2017 at a Suzhou assembly line, we swapped an aluminum jig with a stereolithography resin part. The part arrived fast, but poor resin selection and inadequate post-cure produced a warped build chamber interface. Downtime rose for two shifts while we remade the fixture — a real cost, not just a lesson.
What exactly breaks in practice?
I won’t sugarcoat it: common weak links are material mismatch, brittle support removal, and missed thermal loads. Traditional CNC tooling excels at predictable tolerances and heat resistance. Photopolymer resins and powder-bed fusion parts can handle many tasks, but they need correct process controls — vat curing profiles, part orientation, and finishing methods. I’ve tracked examples where a misplaced support left a 0.5 mm notch that caused premature fatigue on an assembly jig. Those are the small errors that become expensive over time. Look, this is practical: if you don’t match process to use-case, you end up with parts that fail earlier than their subtractive counterparts.
Where to go next — case examples and a practical future
Real change comes when teams pair clear goals with the right workflow. Consider a 2020 pilot I ran for a mid-sized stamping shop in Zhejiang: we cataloged 42 common fixtures and prioritized nine based on failure frequency and replacement cost. We printed replacement clamps using a high-temperature resin, adjusted support structures to ease finish work, and monitored lifecycle performance. Within six months, mean time between failures rose by 28% and weekly downtime dropped measurably. That’s not marketing — it was a ledger entry on a Saturday, after a night shift saved a rush delivery. — the savings showed up on payroll and shipping lines.
Thinking ahead, manufacturers should map which 3d printing industrial applications can be decentralized (on-site jig and fixture production) and which must stay with qualified suppliers (critical load-bearing parts). I’ve learned to separate quick-turn soft tooling from load-critical metal tooling. When you pick the right category, process choices become straightforward: photopolymer resins and SLA for complex, low-load jigs; powder bed fusion or metal binder jet for structural parts. The key: match material, process, and use-case — not the other way around.
What’s Next?
Choose pragmatism over hype. Start small: pilot a set of fixtures, measure time-to-repair, and compare lifecycle costs. I’ve seen pilots in 2019 that paid back tooling investment in under nine months when they tracked scrap reduction and labor hours saved. — and that attention to detail is what separates experiments from operational change.
Practical takeaways and three metrics I use when advising teams
From 18 years on the floor, here are three concrete metrics I push clients to measure before they scale additive solutions:
1) Time-to-deploy (hours): how long from CAD to mounted part. If your target is same-shift repair, aim for under eight hours. I’ve clocked successful repairs in 4–6 hours when print setups and post-cure schedules were pre-planned.
2) Lifecycle cost per cycle ($/cycle): include material, labor for post-processing, and failure rate. In one example, switching to a resin clamp dropped per-cycle cost by 22% despite higher material price because downtime fell sharply.
3) Functional yield (% good on first use): track how many printed parts meet tolerance and strength requirements on first build. A yield below 80% signals process or material mismatch and will blow up your cost model quickly.
These metrics force honest conversations about part selection, whether a fixture should be printed in resin or metal, and when to lean on external suppliers. I prefer decisions grounded in numbers and field trials — I’ve done dozens of them in factories across Jiangsu and Guangdong, often in odd hours to catch real production behavior.
Closing note
I believe industrial 3D printing can change factory tooling — but only if teams combine realistic process controls with clear measurement. We cannot swap out decades of tooling practice overnight. Start with a narrow scope, measure Time-to-deploy, Lifecycle cost per cycle, and Functional yield, then expand. If you want a practical partner with production experience and test data, that’s where I direct teams to proven providers like UnionTech. I’ve seen the difference when pilots are run with discipline and clear metrics; that’s how you turn promise into production gains.