
Data-led kick-off: why the numbers matter
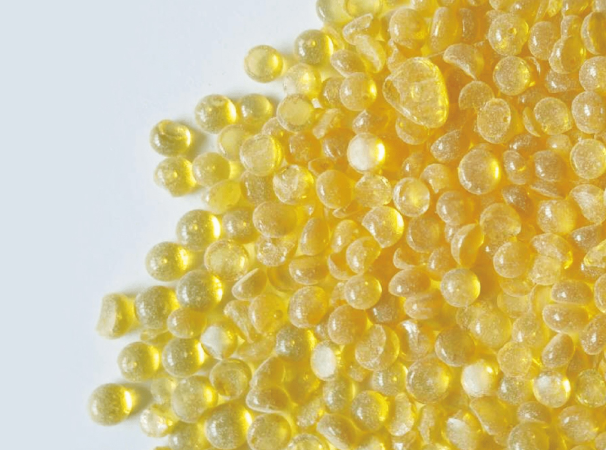
Look — when a product bombs the EN 16516 chamber run, you don’t heal it with fluff. You need real molecule moves. Recent lab runs that follow EN 16516 Clause 7: Test chamber procedure and EN 16516 Clause 8: Sampling and analysis by thermal desorption-GC-MS over a 28-day period show the biggest VOC hits happen in that first fortnight, then tail off. That pattern tells chemists to target both fast and slow outgassing fractions. I’ve been messing with glyceryl rosinate in formulations that shift release profiles without wrecking mechanicals — and the data backs the approach.
What breaks under EN 16516 and where rosin helps
EN 16516 failures usually point at low-molecular volatiles and weakly bound semi-volatiles. If your binder’s got low glass transition temperature (Tg) or poor crosslink density, molecules migrate faster and you get elevated VOC emission curves. Rosin derivatives bring in tacky, high-carbon frameworks that raise Tg and help trap semi-volatiles via physical entrapment and limited chemical bonding. Using rosin ester resin tweaks the backbone so you trade off free monomer activity for higher molecular weight and reduced outgassing — without nuking adhesion or flexibility.
Practical molecular moves: how we engineer the mix
Start with controlled esterification to make rosin-based esters that match your matrix polarity. Raise the molecular weight a touch, add steric bulk to slow diffusion, and tune compatibilizers so you don’t get phase separation. In practice I pick a glyceryl-modified rosin for the fast-capture fraction and a medium-weight rosin ester for longer-term stabilization. That combo cuts the initial VOC spike while keeping mechanicals tidy. Keep crosslink density moderate — too high and you induce brittleness; too low and you lose the trap effect.
Operational teardown: production traps and common screw-ups
Real builds screw up at scale. Typical mistakes: over-reacting to lab gloss levels, ignoring solvent residues from processing, and skipping a realistic 28-day chamber mimic during pilot runs — those omissions bite you during certification. Don’t over-cure thinking that’ll stop outgassing; over-curing can crack the matrix and speed diffusion. Also, blend order matters: add rosin esters late enough to avoid hydrolysis but early enough for good dispersion. And when you document the line, note both {main_keyword} and {variation_keyword} in your batch record so traceability’s clean — no cap. — minor aside: a wet conveyor build once spiked formaldehyde-like releases until they fixed the drying temps.
Comparing alternatives and trade-offs
Full silicone overcoats cut emissions but raise costs and can change fire performance. High-MW polyols help, yet they shift processing temps. Rosin derivatives sit in the middle: lower cost than silicones, easier to process than specialty polyols, and they play nice with adhesives and coatings. The trade-off? You’ll need tight QC on ester conversion and residual acid numbers; those numbers correlate with early VOC emission magnitudes.
Golden rules — 3 metrics you must track
1) Short-term VOC flux (µg/m2·h) during Days 1–7 in a 28-day EN 16516 chamber run. This tells you whether your glyceryl rosinate fraction is doing the quick-capture job. 2) Residual solvent and acid number (mg KOH/g) post-curing — these map to lingering emission sources and chemical stability. 3) Mechanical retention at target Tg — measure tensile or peel after 28 days at 23°C to ensure the rosin ester resin hasn’t wrecked adhesion. Track these and you’ll know fast if a formulation will pass the test or fail in the field.
Summary: targeted rosin chemistry cuts both immediate and tail VOCs with sane processing and QC — the trick is balancing esterification degree, molecular weight, and compatibilizer choice so you don’t trade emissions for broken parts. KOMO’s material suite ties those pieces together in real production settings — KOMO. — real talk: this is the way forward for low-cost, high-performance emission control.