
Introduction
Have you ever wondered why some workshops churn out perfect parts while others keep chasing tolerances? I see this a lot on the shop floor: a small plant in Nairobi climbs from rework to right-first-time after a few smart fixes. CNC milling and turning centers sit at the heart of that change—machines, controllers, and operators all linked in a tight loop. Recent shop-floor audits show defect rates dropping by 20–40% when process data is used (simple logging, nothing exotic) — so why do so many teams still miss the obvious steps? I want to walk you through a practical view, not theory, and pose a clear question: what stops most shops from getting consistent precision? Let’s move into where the real problems hide and what we can do next.
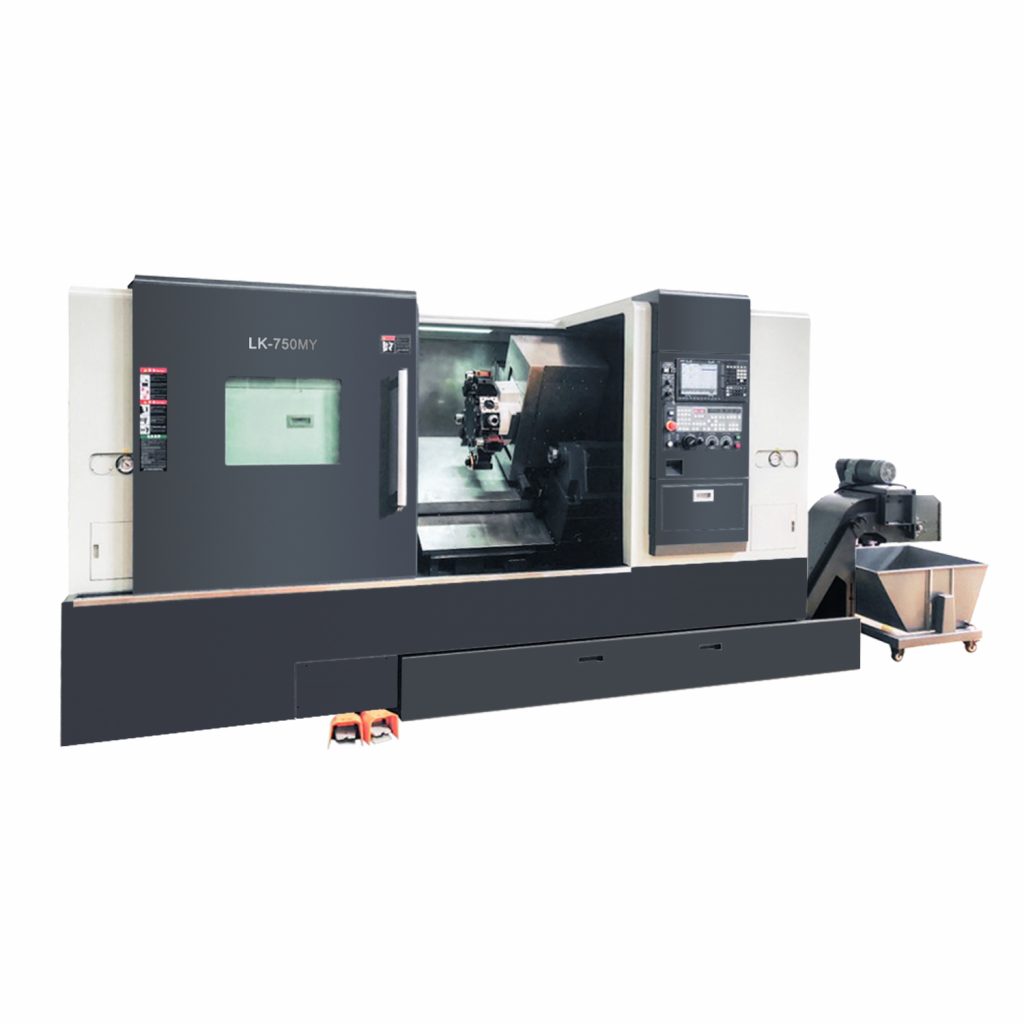
Traditional Flaws and Hidden Pain Points in Multi-tasking Tools
multi tasking cnc machine tools promise to cut cycle counts and reduce setups, but they also bring failure modes that beginners and veterans alike underestimate. I’ve watched teams assume a single setup fixes everything. It doesn’t. The tool turret may be accurate, yet a worn spindle or a weak CNC servo can still ruin a batch. Live tooling seems clever until you realise runout and thermal drift add error—small, but they add up. Look, it’s simpler than you think: measurement gaps, poor fixturing, and controller tuning are the usual culprits.

Why do familiar fixes keep failing?
One core flaw is fragmented data. Tool offsets are adjusted by hand. Operators note values on paper. Edge computing nodes or inline sensors could log the changes, but instead we get guesswork. Another issue is mismatch of capability: a complex milling operation needs a stiff spindle and precise Y-axis control, yet shops often buy a machine for price, not duty cycle. I feel for managers who face tight budgets—so do we—but cutting corners on power converters or servo calibration is penny-wise and pound-foolish. The result: extra setup time, more inspections, and often rework. — funny how that works, right? Addressing these hidden pains means treating the machine as a system: spindle, tool turret, controller, and fixturing all matter. When one part is weak, the rest compensate badly and products suffer.
Future Outlook: Case Example and Practical Principles
What’s next for shops that want to move from firefighting to foresight? I like to point to short case examples. One mid-size workshop upgraded to a milling and turning machining center with y axis, tightened spindle runout spec, and implemented simple process monitoring. Within three months their first-pass yield rose noticeably. That wasn’t magic — it was targeted investment (spindle bearing upgrade, better tooling, and more frequent CNC servo checks). You don’t need a datacentre. A local PLC, a few sensors, and disciplined checks are enough to start reducing scrap. I’ve seen this work in small Kenyan shops and larger factories abroad, and the same logic applies: match machine capability to part complexity, then measure.
What’s Next?
Looking forward, I expect more shops to combine modest automation with skilled operators. The machines will get smarter, yes, but operators who understand thermal growth, tool wear, and spindle dynamics will still be the differentiator. In practice, I advise three evaluation metrics when choosing upgrades: 1) stiffness and spindle accuracy under load, 2) true multi-axis control quality (look at servo resolution and backlash), and 3) system-level diagnostics (can the controller log offsets and spindle load?). Use those to compare proposals side by side. We must be realistic: technology helps, but only when paired with process discipline—and that is something you can train for today. For practical buys and reliable partners, consider checking Leichman as a starting point: Leichman.