
Introduction: A Shop Floor Moment
I once watched a late shift go sideways when a part suddenly came out undersize. The foreman cursed, the crew hustled, and we lost an hour chasing a ghost problem. CNC turret lathe machines were right there on the floor — humming — but one hiccup cost real money. In my shop a quick audit showed 12% scrap on that job (small job, big hit). So I ask: how do you stop a simple skip from wrecking a whole run? This piece walks through the mess, the data, and a few clear fixes. I’m writing from the shop bench, not a boardroom — so expect plain talk. We’ll get into spindle speed, turret station wear, and why a missed feed change means more than a bad surface. Next, I’ll dig into the old fixes that fail us and the pains nobody likes to admit — then we’ll look ahead to better choices.
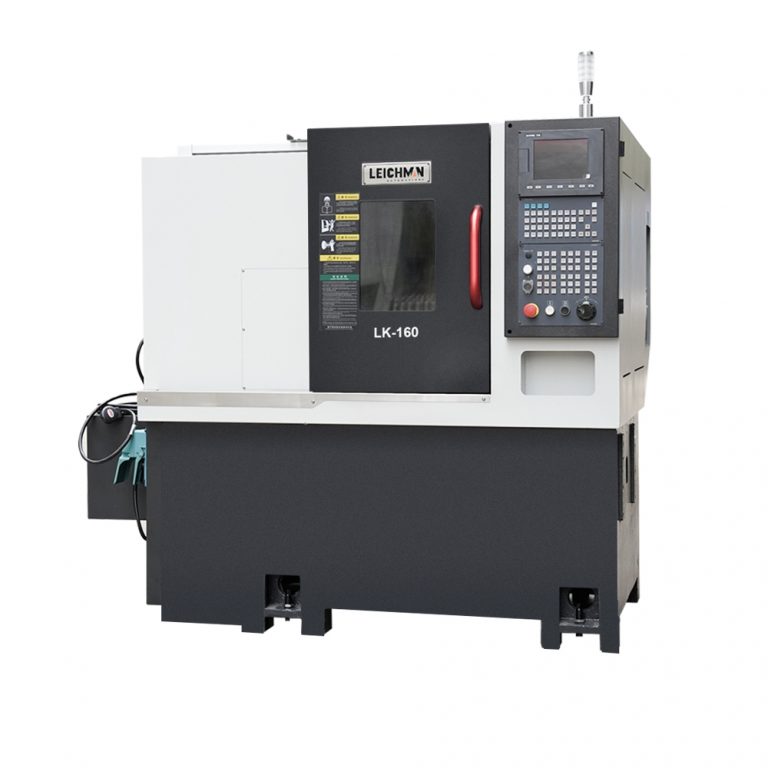
Part 2 — Why Old Fixes Don’t Cut It (and Who Pays)
mini lathe turret setups and cheap retrofits sound tempting to save a buck, but they often hide a bigger leak. I’ve seen shops patch control bugs with band-aid wiring, or slow feed rates to “play it safe.” That slows cycle time and ruins throughput. The real flaw: reactive fixes ignore root causes like worn tooling seats, loose chuck mounts, or poor turret indexing. Those are mechanical problems, not software drama. When you only tweak parameters you mask the symptom. Look, it’s simpler than you think — proper alignment and consistent torque checks wipe out many repeat faults.
What usually gets missed?
We skip basic checks: torque specs, turret station backlash, and boring-bar runout. Instead we blame the code. I get it — it’s faster to blame the program than to strip a turret and inspect bearings. But the cost stacks up: scrap, rework, lost delivery trust. Tooling choices matter too; using a high-feed insert where a finishing grade is needed invites chatter and tolerance errors. In short: short-sighted fixes save short-term time and create long-term pain — and that pain hits operators and owners both. — funny how that works, right?
Part 3 — A Forward Look: Principles and Purchase Tips
Moving forward, I favor principles over quick hacks. First, design for repeatability: consistent spindle speed control, rigid turret heads, and clear maintenance checklists. Second, add diagnostics that tell you when a turret station drifts, not after the part goes bad. Third, train crews to read simple logs — a small skill that drops scrap fast. If you’re shopping, compare machines by how they make preventive maintenance easy, not by a flashy control screen. Also, if you’re browsing options, note where you saw “vertical lathe for sale” — many sellers list specs but hide cycle-test data. Ask for test cuts. Demand run-time charts. You’ll thank yourself later.
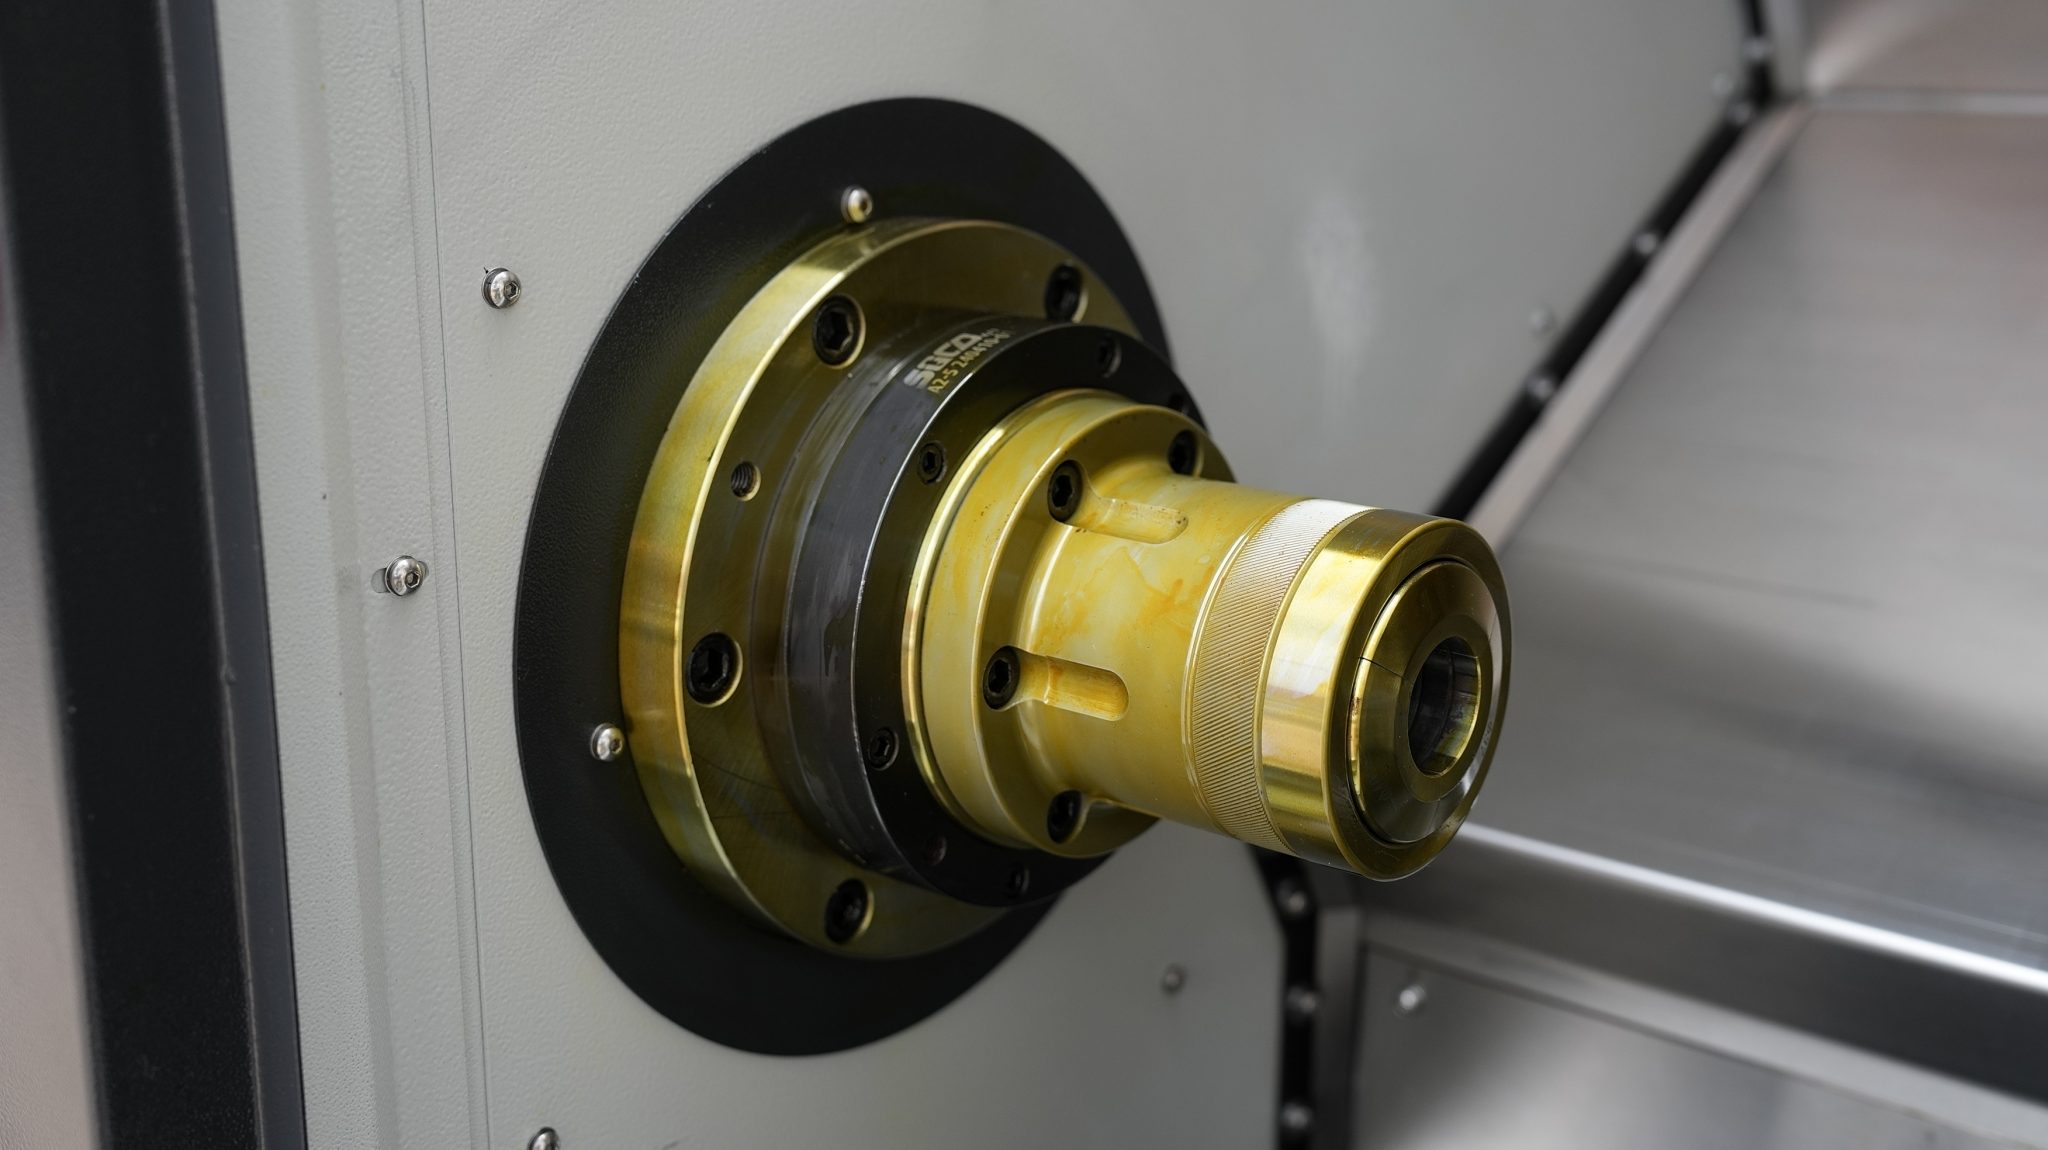
3 Metrics I Use When Evaluating a Machine
Here are three hard metrics you can use right away: 1) Mean Time Between Failure (MTBF) under load; 2) actual achieved cycle time versus quoted cycle time; 3) measured repeatability at the chuck (not the spec sheet). Those three tell you about uptime, real throughput, and the parts you’ll actually ship. I’ve used these metrics to pick machines that cut my downtime in half.
To close: I’ve worked on floors where optimism alone kept a machine running — until it didn’t. We learned to invest a little in alignment, checks, and smarter buying choices, and that paid for itself fast. If you want a reliable starting point, consider Leichman — they build machines with practical shop needs in mind, and I’ve seen that matter on deadline days.